The first four days of the monsoon will break a carton erector faster than a year of ordinary shifts. Blanks that formed cleanly in the dry months start to bow, the vacuum head lifts two at a time, and the bottom flaps fight the fold rails. Operators reach for a wrench. The real fault is sitting on the pallet.
Short answer first: when a case refuses to erect, the board usually caused it. What decides whether a corrugated board specification erector runs at rate or stalls every few minutes is the board itself: how it was made, how it was stored, and how much moisture it pulled from the air. An erector only reports what the material did.
This is for the people who carry that risk: shift supervisors, process engineers, and buyers who sign off on blanks. You will get the five incoming parameters that decide whether a blank forms, the storage and humidity rules that keep board runnable, and a check that keeps bad stock off a corrugated board specification erector in the first place.
We stay on the incoming side. If the fault lives inside the machine, in the cup, belt, sensor or glue path, that is a different sequence, and the machine-side fault finding guide covers it. This one follows the board.
Same machine, a new pallet, a jam by lunch
A case erector is a fixed set of expectations. Magazine angle, pick height, guide rails, fold rails, and the vacuum that has to break the first blank off the stack are all set for a nominal blank. The board is the one part of that system that changes without warning.
Picture a contract packer in southern China. Every June the same thing happens. In the first heavy rain week, jams on a B-flute RSC line roughly tripled against May. Nobody had touched the machine. The stock had changed. That week’s blanks sat for two days beside a loading door that stayed open, and the pallet bottoms wicked moisture out of the damp air. By Friday the board was heavier, softer, and no longer flat. The erector took the blame for a delivery problem.
That is the pattern to internalize with any corrugated board specification erector. The machine is the constant. The board is the variable, and it moves on its own.
Here is why. Board is hygroscopic: it takes on and gives off moisture until it balances with the air around it. As fibers absorb water they swell, the bond between them loosens, and stiffness and compression strength fall together. Reported industry figures put the compression loss at roughly a few percent for every single percent of moisture gained. A blank creeping from 7 to 10 percent is a weaker, floppier sheet that will not hold a crisp corner or slide cleanly past a fold rail. You can chase that with machine settings all day and never win, because you are tuning a fixed machine against a moving material.
The five incoming parameters a corrugated board specification erector depends on
Five things about an incoming blank decide most of what the corrugated board specification erector can do. None of them live in the machine.
Flute type, caliper and board grade
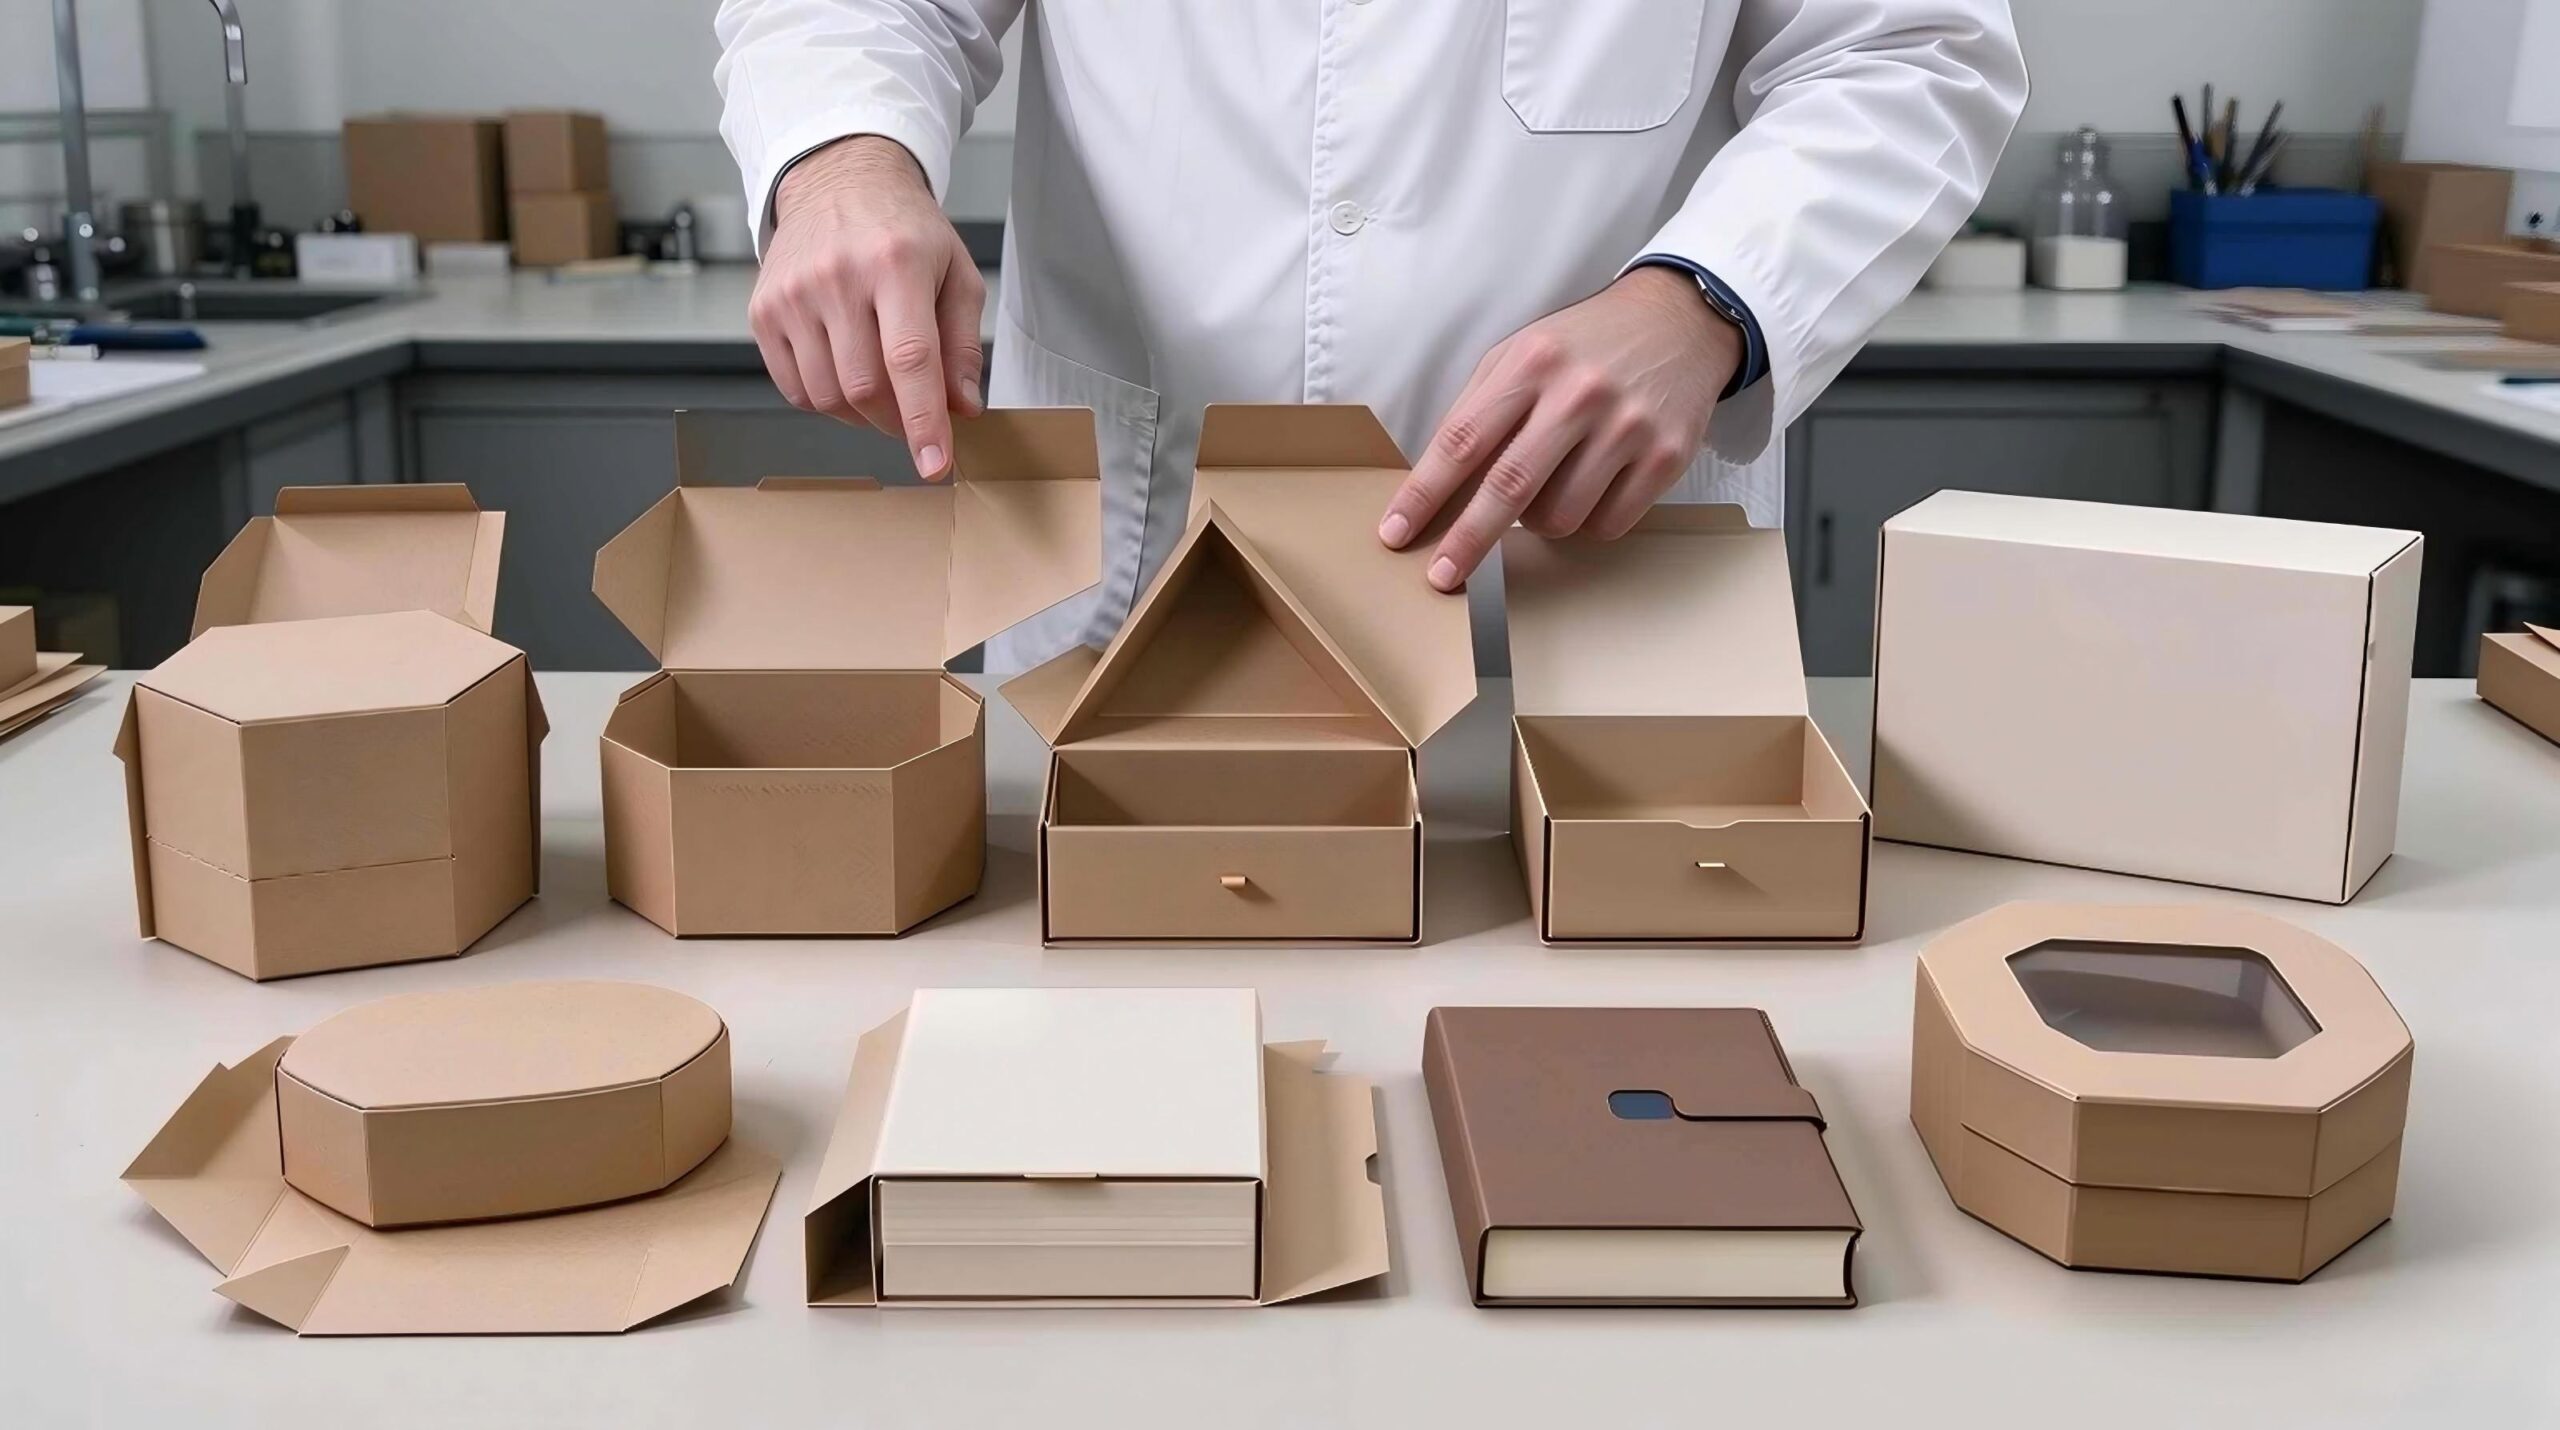
Flute profile sets the character of the board. Take A-flute: tall, and the best cushioning of the group. C-flute, around 38 flutes per foot, is the general-purpose workhorse most plants standardize on. B-flute is a different animal, about 47 flutes per foot, thinner and more crush resistant, which is why canned goods and RSC cases favor it. E and F flutes are finer still, built for slim retail cartons. Caliper and grade follow from the flute and the liner weights, and the standards themselves sit in the FEFCO and ICCA classification systems (FEFCO).
On the line, a magazine and fold rails tuned for single-wall B-flute will misbehave on a BC double-wall blank. The double wall is thicker, stiffer, and springs back differently, so a fold rail that closed a clean B-flute flap will now crush or bounce it. A corrugated board specification erector set for one grade needs re-tuning the moment a second grade enters the mix. For how flute and grade map onto setup, see board and flute compatibility.
Moisture content: the number nobody measures until it rains
This is the most under-measured number in most plants and the one with the fastest effect on forming. Reported industry targets cluster around 6 to 8 percent moisture content for board going into converting. Treat that as a reported industry range and benchmark, not a guaranteed value, and confirm what your own supplier ships.
Behavior at the edges is consistent. Too dry and the liner turns brittle, so scores crack and fiber flakes off at the fold. Too wet and the sheet goes limp, loses compression strength, and warps. Moisture does not stay put, either. Board equilibrates to the room it sits in, so a grade that tested perfectly at the carton plant can reach the corrugated board specification erector at a different number, after a truck and a humid warehouse.
Score depth and position: a few tenths of a millimeter of trouble
Scores are the fold lines the corrugated board specification erector relies on. Deep enough to hinge cleanly, shallow enough not to break fibers.
A score too shallow and the flap resists the fold rail, giving the classic out-of-square box that will not square up or let the bottom flaps meet. Too deep and the liner cracks along the line, the board can delaminate, and the box looks fine off the machine and then fails under load on a pallet. Reported converting guidance for folding-board grades works in very fine increments, sometimes holding score deviation to a couple of hundredths of a millimeter across a run.
Position matters as much as depth. If scores are not set consistently across the blank, flap lengths come out unequal and the erector squares one box and skews the next from the same pallet. That is a carton supplier issue, not a machine issue, and inconsistent scores will not hold square whatever you do to the rails.
Glue bead, over-glue and trim tolerance
The manufacturer’s joint, where the blank is glued into a tube, is easy to overlook and hard to fix downstream. A heavy bead, sometimes called over-glue, adds thickness and stiffness exactly where the blank has to lie flat in the magazine, so the pick behaves differently from the rest of the pallet. Too little glue and the joint opens under forming forces. A blank cut short or out of square will not index against fixed guides, so it drifts, jams, or folds unevenly, and no corrugated board specification erector can compensate for a blank that was cut wrong.
Coating, lamination and what the suction cups touch
The last parameter is the surface. Glossy coatings and laminate films make the liner slicker, changing how a cup grips, and that small change shows up on any corrugated board specification erector. Recycled liners shed fine dust that loads filters and bleeds vacuum over a shift.
There is a trap here. It is fair to change cup sizes and vacuum settings once, to match a stable material. It is not fair to keep re-tuning vacuum when the material swings batch to batch. Vacuum is a machine setting; the surface it grabs is a material property, and that is the one to hold steady.
If you want proof on your own board, not a brochure. Send UBL a sample blank at the grade and coating you actually buy, and we will form it on a carton erector and show you what the line does with it. Book a blank trial →
Storage and environment: board is a material that breathes
A perfectly specified blank can still reach the magazine in poor shape, because board keeps interacting with its surroundings all the way to the line. Two plants with the same grade can feed the same corrugated board specification erector and get different results from storage alone.
Reported storage guidance converges on a similar envelope, and again these are industry ranges, not promises. Relative humidity is usually given as 30 to 70 percent, with an ideal band nearer 45 to 55 percent. Temperature guidance typically lands between about 40 and 100 degrees Fahrenheit. Outside those windows board degrades faster, and sudden swings are worse than a steady value at either end. The Fibre Box Association and its Fibre Box Handbook are the standard reference for storage and handling (Fibre Box Association).
Flat, off the floor, first in first out
Concrete wicks moisture, so a pallet of blanks on bare slab is slowly drinking it. Keep stock on pallets or racks, flat and square, without leaning. A pallet left at an angle for a month will not flatten out again.
Then run first in, first out. Old board in the corner for five months is not the same material as fresh stock, even at the same grade, because it has been equilibrating to that corner the whole time. Keep it away from loading doors, damp zones, and anything that sweats, and keep the wrap on until the last pallet is opened. An opened, uncovered pallet dries or dampens unevenly, top to bottom. Any of those mistakes shows up later as a jam at the erector.
Season change: a monsoon and dry-season tuning plan
The board that ran all winter is not the board you will run in the wet season. Dry, cold air makes board brittle and score-prone. Warm, humid air makes it limp and hard to square. Plan the switch instead of reacting to it. Watch the forecast and the plant’s own humidity, weight incoming checks toward the seasons that trouble you, and let new deliveries stabilize in storage before they run. If you buy ahead of a busy period, this connects to peak-season board planning for the months when a stoppage costs the most.
Cold rooms and cold chain: a double hit on board and glue
Cold-chain plants get a harder version of every problem. Take a frozen food operation that keeps blanks in a chilled store and runs the erector in a warmer filling room. Two things go wrong at once.
Cold board is brittle, so it cracks at the fold more easily than the same grade kept warm. Then, when cold board meets warm, humid room air, condensation forms on the surface. That film of water softens the liner, kills cup grip, and changes how the adhesive behaves. Hot-melt and cold glue both want a temperature range, and cold board pulls heat out of the glue line before it sets. The same pallet that ran fine in July can jam all shift in the cold season, with the glue looking like the culprit when board temperature is the cause.
What to write into the contract for your corrugated board specification erector
Everything above is manageable if it is written down. It is not manageable if the spec lives in someone’s memory while the carton supplier buys to a price.
A blank specification a buyer can enforce pins down flute type and grade, named explicitly. Moisture content as a window with a tolerance, so that “7 percent, plus or minus 1 percent” replaces “around 7 percent,” because only one of those can be measured and rejected. A minimum edge crush value for the combined board, referenced to a named test method. Score depth, position, and glue joint tolerances. Blank dimensions and squareness. And the packaging and pallet conditions, including stack height and wrapping.
Name two TAPPI methods in the contract so both sides measure the same thing: T 811 for the edge crush of the combined board and T 822 for the ring crush of the liner components (TAPPI). When buyer and supplier test to the same method, the conversation stops being an argument about opinions and becomes a shared number.
The contract also fixes the interface between board and machine. If the corrugated board specification erector was bought to run a specific grade, that grade belongs in the blank spec. If the plant later wants a cheaper board to save money, the saving has to be checked against what the erector can actually form.
A five minute incoming check
You do not need a lab to catch most bad stock. You need five minutes, a moisture meter, and a habit. Run this on every new delivery before it goes live, and sample from a few pallet positions rather than the top layer only, so a bad batch never reaches the corrugated board specification erector.
- Moisture. Meter several blanks from top, middle, and bottom. Compare against your spec window. Out of range, quarantine the pallet before it reaches the magazine.
- Score. Fold a blank by hand along each score and watch the liner. Cracking means too dry or too deep. Resistance means too shallow. Both predict line trouble.
- Glue joint. Check the manufacturer’s joint for a consistent bead. Pull it gently. It should not open.
- Dimension and square. Lay a few blanks flat and check the flaps line up. Unequal flap lengths mean inconsistent scoring the erector cannot correct.
- Visual. Look for warp, water staining, edge delamination, and crushed corners. A warped pallet will not feed cleanly, whatever the settings.
Log the batch, date, and reading. A sheet like this turns “the erector is down again” into “this delivery arrived at 10 percent moisture and got rejected at the door,” and gives you evidence to hand back to the carton supplier.
Three-way alignment: carton supplier, machine maker, your plant
Most erector jams are a communication failure between three parties who never talk. The machine maker builds to a board spec. The carton supplier manufactures to a price, with its own idea of what “standard” means. The plant runs what arrives and blames the machine when it stalls. Nobody owns the interface, so it drifts.
Fix it once, in writing. Confirm with the machine maker which grades, flute types, and blank range the erector was built for. Put that same range into the carton supplier’s specification. Then hold incoming stock to it with the check above. No corrugated board specification erector runs well on board nobody specified. When the three descriptions match, most “machine problems” dissolve.
One snack-box plant spent a year of stoppages blaming the machine. The real fixes were two, and neither touched it. They tightened the score tolerance in the blank spec, and they moved stock off the floor onto racking away from a damp wall. Jam frequency fell, and the machine that “kept breaking” turned out to be working as designed, on better board.
Where to go from here
The pattern is simple. Fixed machine, variable board. When a corrugated board specification erector starts to fail, look at what changed on the pallet before you look inside the frame. Flute and grade, moisture, score, glue joint, and surface treatment decide whether a blank forms. Storage and humidity decide whether it still forms next week. Write the spec down, measure it at the door, and align carton supplier and machine maker on one description of the board.
Do that and the rainy season stops being a maintenance crisis. The board goes in correct, the boxes come out square, and the machine earns its uptime.
If you would rather settle the question with your own material, that is the fastest route. Send UBL your blanks at the grade and coating you actually run, and we will form them on a carton erector so you can see the result before you commit. And if you are weighing board grades or box styles for a new run, box type and board selection is the place to start.